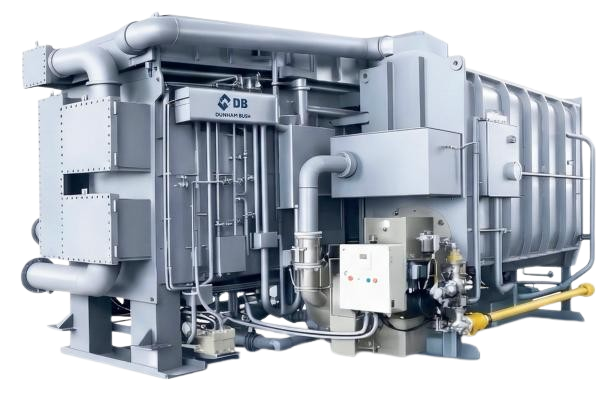
Designed with double-stage evaporation technology, advanced anti-crystallization protection, automatic air purging, and intelligent monitoring to ensure reliable, stable, and energy-optimized performance across all load conditions.
Key Features
High efficiency double-stage absorption technology
Direct-fired natural gas operation
Advanced anti-crystallization protection system
Automatic air purging & vacuum protection
Intelligent monitoring with optimized part-load performance